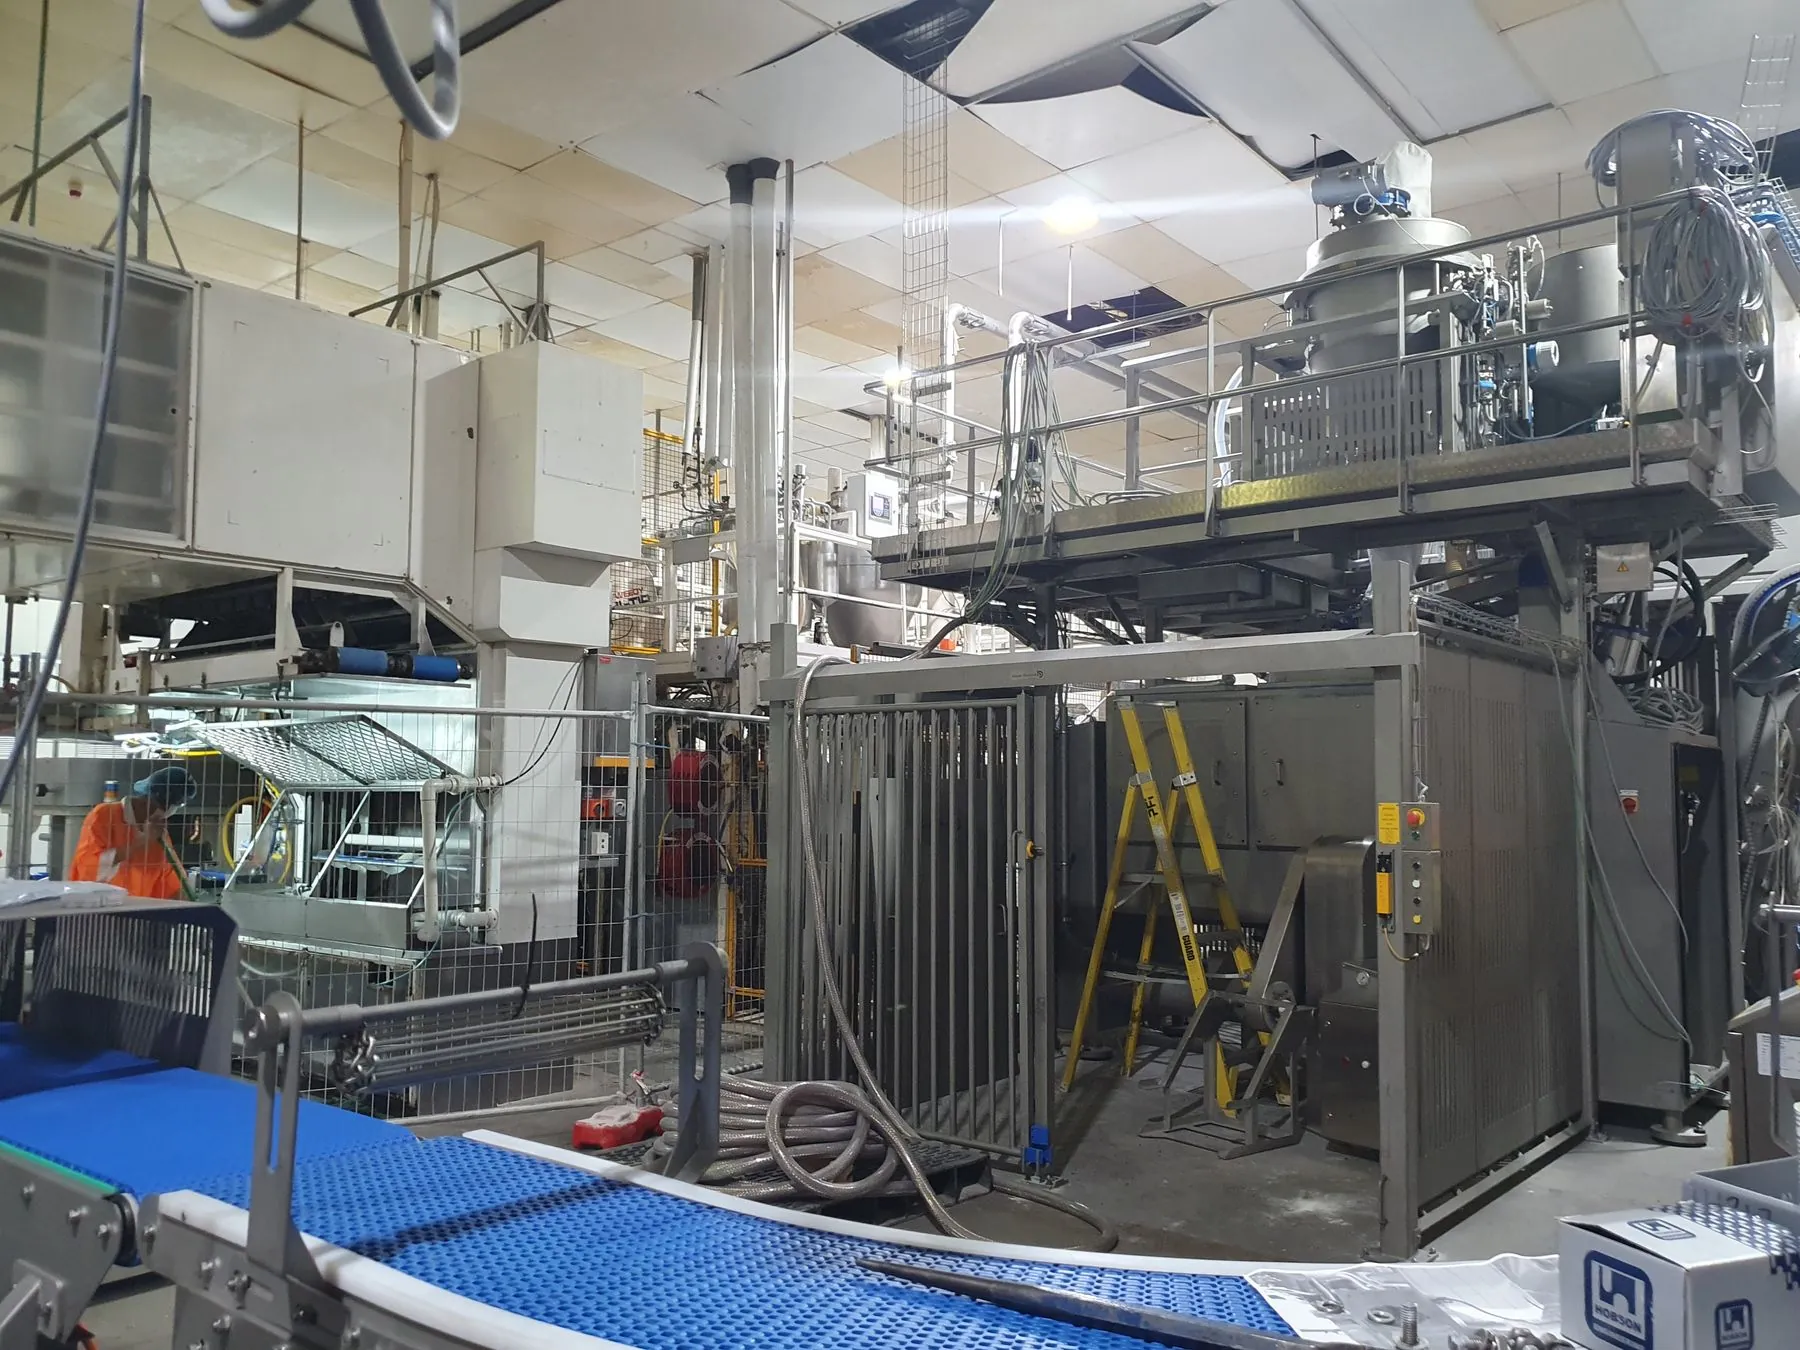
Food and beverage electrical maintenance
Production line breakdowns, planned maintenance, shutdown support and controls work on food and beverage sites, carried out around how the plant actually runs.
Electrical maintenance and project work on food production, manufacturing and processing sites across South East Queensland.
The environment
Electrical work with production waiting
Most of our work is on food and beverage sites, and it is where the twenty years behind Sparktech was spent. It is a particular environment to work in, and it shapes how electrical work has to be done.
Lines run long hours. Product is perishable or time-critical. Washdown and hygiene requirements affect what can be opened and when. Access windows are short and often at night. A fault on a packaging line does not just stop a machine, it backs up everything upstream of it.
What we get called to
Faults on food production plant
Production line stoppages
Faults that have taken out a machine, a conveyor or a whole line, diagnosed methodically rather than by swapping parts.
Process and packaging equipment
Electrical fault finding on process equipment, packaging machinery, checkweighers and downstream handling.
Conveyors and handling
Drive faults, motor and gearbox electrical issues, sensors, and the control circuits that stop and start plant.
Motors and drives
Motor fault finding, insulation resistance testing, starters and overloads, drive fault finding and parameter configuration.
PLC controlled machinery
Establishing whether a fault is electrical, in a field device, in a drive, or control related, and going online to diagnose.
Ovens and production machinery
Electrical work on ovens, provers, mixers and the machinery that runs the line.
Working around production
The window is usually the constraint
On a food site, when the work happens matters as much as what the work is. Very little can be done during a run, so electrical work gets pushed into cleans, changeovers, night shift or a planned shutdown.
- Work scheduled into cleans, changeovers and planned downtime where possible
- Night shift and weekend attendance where the line cannot stop during the day
- Shutdown electrical work scoped and prepared before the plant stops
- Hygiene and washdown requirements accounted for in how work is carried out
- Coordination with the site maintenance team and other trades
- Site inductions, permits, isolation and lockout to the site's own procedures
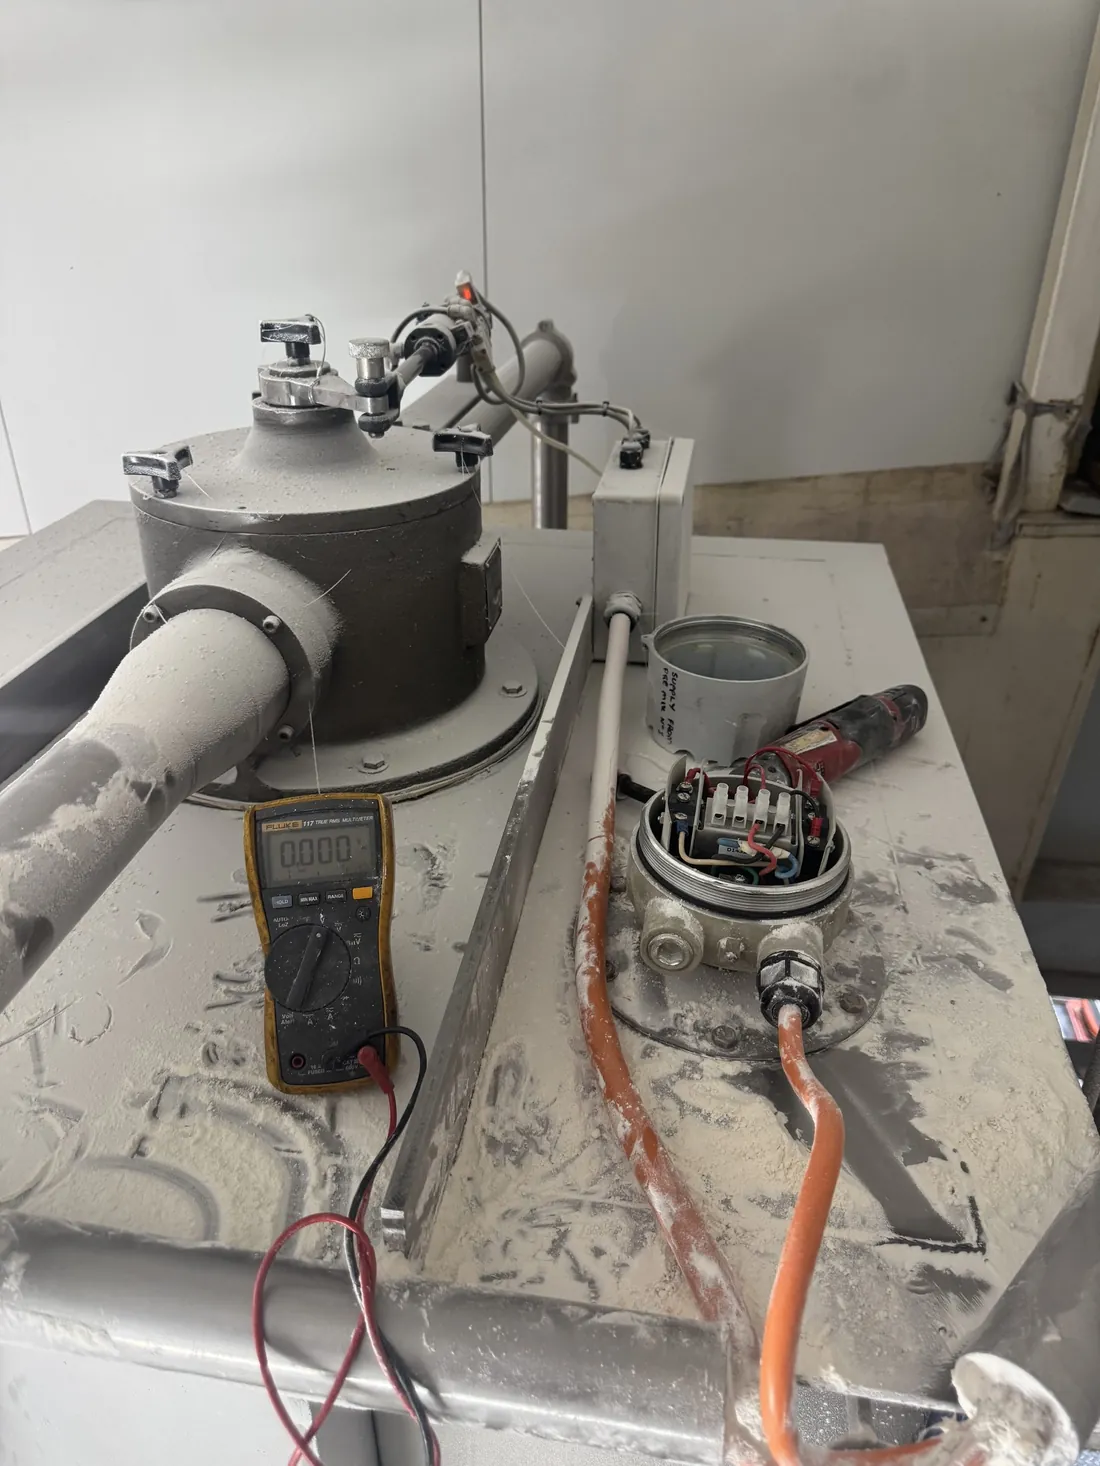
Where a site has classified areas around combustible dust, our EEHA competencies cover installation, inspection and maintenance within them.
Read more
Case studies from food production sites
CompactLogix replacement and firmware upgrade
A failed comms port left the HMI with no control. Goodman Fielder, Burleigh Heads.
Chilled water solenoid fault
Traced through the control program to a fuse hidden behind an output module.
Cimcorp energy chain replacement
Energy chain and cables replaced inside a 24-hour shutdown window.
Get in touch
Talk to us about your site
Tell us the site, the plant involved and what is happening.
0434 059 952For breakdowns and after-hours requirements, call to check current availability.